Top 10 Plastic Injection Machine Parts for Buyers
Buying the right plastic injection machine parts is not just a matter of comparing prices. A small mismatch can affect cycle stability, surface finish, energy use, and unplanned downtime. A worn check ring may cause inconsistent shot size. A poorly matched heater band can leave temperature zones uneven. These details matter on the factory floor.
John Bozzelli, a recognized scientific-molding specialist, offers a useful reminder: “Measure the process before blaming the part.” Buyers should assess fit, material, operating conditions, maintenance needs, and supplier support—not rely on appearance alone. A polished screw or nozzle can still be the wrong specification. Even experienced teams sometimes overlook compatibility.
This guide covers ten commonly purchased components, from screws and barrels to hydraulic pumps, servo motors, heaters, and seals. For each, it highlights what to inspect, which questions to ask, and where replacement choices can influence performance. Check drawings, machine manuals, and wear records before ordering. Ask suppliers for dimensions, material details, and relevant test information. Compare carefully. A part that seems inexpensive today may require more maintenance tomorrow. And not every upgrade pays off; the actual result depends on the machine, resin, and process.
What Are the Main Parts of a Plastic Injection Machine?
Top 10 Plastic Injection Machine Parts for Buyers
What Are the Main Parts of a Plastic Injection Machine?
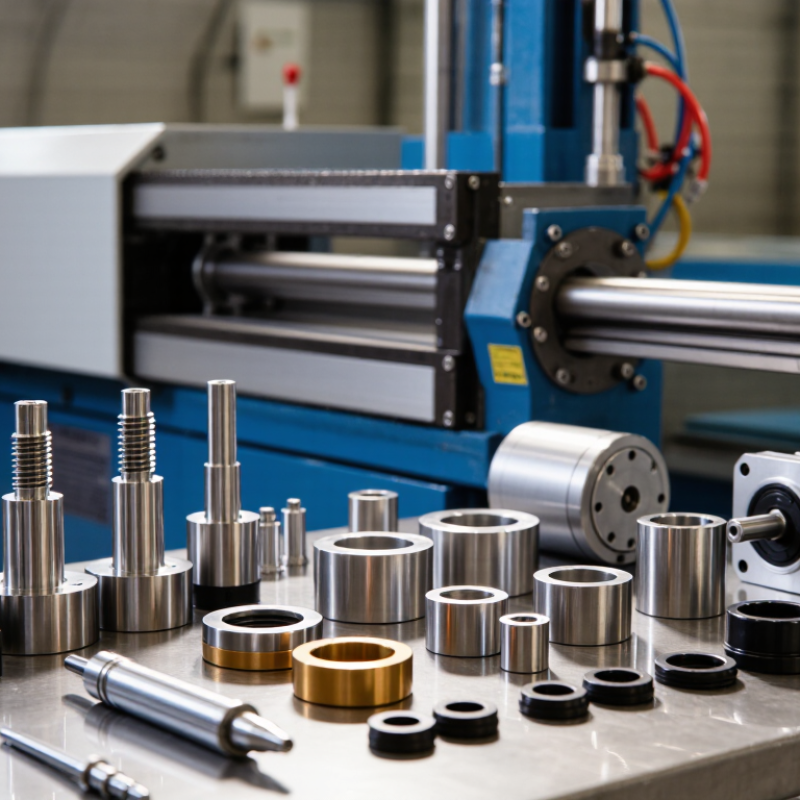
A plastic injection machine has several coordinated units. The injection unit includes a hopper, heated barrel, reciprocating screw, and nozzle. Pellets drop from the hopper into the barrel, where heat and screw movement melt them. The screw then pushes a measured shot through the nozzle and into the mold. Uneven melt temperature can cause inconsistent parts, so barrel zones and screw condition matter.
The clamping unit holds the mold closed under pressure while plastic fills and cools. Its main components include the fixed and moving platens, tie bars, and clamping mechanism. Inside the mold, cavities shape the product; cooling channels help remove heat, and ejector pins release the finished part. A hydraulic or electric drive powers machine movements, while the control system monitors settings such as temperature, pressure, and cycle time. Small sensor errors can still affect production.
Tips: When comparing machines, check shot capacity, clamping force, and mold dimensions against your actual parts. Ask how maintenance access works. A worn screw or leaking nozzle may be easy to overlook during a quick inspection.
How the Injection Unit Melts and Delivers Plastic
Inside an injection molding machine, the injection unit turns solid pellets into a controlled stream of molten plastic. Pellets fall from the hopper into a heated barrel, where rotating screw flights carry them forward. Heater bands warm the barrel, but friction from the screw also adds heat. Both matter. Relying on heaters alone can create uneven melt conditions.
The screw has distinct zones for feeding, melting, and metering. As it rotates, pellets soften and mix; the screw then moves backward as a measured shot gathers ahead of its tip. A check valve helps prevent melt from flowing backward during injection. When the screw advances, plastic passes through the nozzle and into the mold. Timing is critical. A worn check valve may cause inconsistent shot size, even when the machine settings appear unchanged.
Buyers should inspect screw and barrel wear, heater response, nozzle condition, and the injection drive. Ask how the unit handles the intended resin and shot size, not just its maximum capacity. Watch for temperature variation along the barrel and hesitation at the nozzle. Small details count. Even a well-maintained unit needs setup adjustments when material, mold, or production conditions change. Calibration is useful, but it is not magic.
How the Clamping Unit Secures and Opens the Mold
The clamping unit keeps the mold halves aligned against injection pressure, then separates them for part removal. Its main parts include the stationary platen, moving platen, tie bars, and a toggle or hydraulic drive. During closing, the moving platen travels along the tie bars until the mold faces meet. The unit then applies enough force to resist cavity pressure and limit flash. Too little force can let plastic escape at the parting line; excessive force can strain the mold and machine. Small misalignment matters. PlasticsEurope’s Plastics—The Fast Facts 2023 reports 400.3 million tonnes of global plastics production in 2022, underscoring the scale of processing behind everyday molded products.
Clamp force is commonly estimated from projected part area and cavity pressure, but that calculation is only a starting point. Material, wall thickness, gate design, and machine condition also affect the setting. In production, technicians check parting-line flash, tie-bar balance, and mold protection settings during setup. Once the hold and cooling stages finish, the clamp opens in a controlled stroke; the ejection system can then release the part. Smooth opening helps prevent sticking and unnecessary mold wear. A practical caveat: tonnage readings alone do not prove that the mold is closing evenly. A slightly imperfect setup can still produce parts, but recurring flash or uneven wear deserves investigation.
Top 10 Plastic Injection Machine Parts for Buyers - How the Clamping Unit Secures and Opens the Mold
| No. | Part | Main Function | How It Helps Secure or Open the Mold | Buyer Checks |
|---|---|---|---|---|
| 1 | Fixed Platen | Supports the stationary half of the mold and connects it to the machine frame. | Provides a rigid mounting surface that keeps one mold half in position during clamping and injection. | Check platen dimensions, mold-mounting hole pattern, flatness, and compatibility with the mold base. |
| 2 | Moving Platen | Supports the moving half of the mold and travels along the clamping unit. | Moves the mold halves together to close the mold and apart to open it after the molding cycle. | Review platen size, travel, guidance arrangement, and permitted mold dimensions. |
| 3 | Tie Bars | Connect the platens and carry tensile loads generated during clamping. | Help resist mold-separating forces and maintain the clamping structure under load. | Check tie-bar spacing, usable distance between bars, condition, and whether the mold can fit through the opening. |
| 4 | Toggle Links and Link Pins | Form the articulated linkage used in a toggle-type clamping mechanism. | As the linkage approaches its straightened position, it generates and holds clamping force; reversing the motion opens the mold. | Inspect for wear, looseness, lubrication needs, and smooth operation throughout the opening and closing stroke. |
| 5 | Clamping Cylinder | Uses hydraulic pressure to drive the clamping mechanism in hydraulic or hybrid designs. | Supplies force to close the mold and, depending on the machine design, initiate mold opening. | Check rated pressure, cylinder condition, seal leakage, and the machine's clamping-force range. |
| 6 | Clamping-Force Adjustment Mechanism | Adjusts the clamping unit to accommodate different mold heights. | Sets the mechanism's working position so the mold can be clamped correctly across its supported height range. | Confirm the mold-height adjustment range, adjustment method, and suitability for the intended mold thickness. |
| 7 | Platen Guides and Bushings | Guide the moving platen as it travels and help control its alignment. | Support consistent mold opening and closing and help the mold halves meet in alignment. | Check guide condition, lubrication requirements, wear, and platen movement for binding or excessive play. |
| 8 | Mold-Height Adjustment Drive | Moves the adjustment mechanism to suit the installed mold thickness. | Allows the clamping unit to be set for a mold so it can close and develop clamping force within the machine's operating range. | Check the supported mold-height range, adjustment speed, and whether adjustment is automatic or manual. |
| 9 | Ejector System | Drives ejector pins or plates in the mold to release the molded part. | Operates after mold opening; it does not generate clamping force, but it is an essential part of the mold-release sequence. | Compare ejector stroke, available force, rod or coupling arrangement, and timing controls with the mold requirements. |
| 10 | Mold-Protection and Position-Sensing Components | Monitor platen position and support controlled closing and opening sequences. | Position feedback and low-pressure mold-protection settings can help detect an obstruction or incorrect closure before full clamping force is applied. | Review sensor function, closing-speed settings, low-pressure protection capability, and safety interlocks. |
Note: Clamping-unit layouts and specifications vary by machine design. Confirm mold dimensions, required clamping force, mold height, opening stroke, and ejector requirements against the machine manufacturer’s technical documentation.
Top 10 Plastic Injection Machine Parts Buyers Should Know
A buyer should understand the parts that control feeding, melting, and injection. The hopper stores resin; check its lid and throat for dust or moisture. The screw moves and melts material inside the barrel. Look for wear, scoring, and dimensions suited to the resin. The non-return valve helps maintain a consistent shot. If it leaks internally, part weight may vary. The nozzle transfers melt into the mold, so its tip and seating surface matter.
Heater bands warm the barrel zones, while thermocouples monitor their temperatures. Ask how each zone is tested, not only whether it powers on. The injection carriage presses the nozzle against the mold. Its movement should be smooth, without obvious looseness. The drive system, hydraulic or servo-electric, supplies motion and pressure. Compare service access, response, and energy needs with your production cycle. Details on a specification sheet can sound reassuring. They do not replace inspection.
The clamp unit holds the mold closed; check platen condition and opening stroke. Tie bars guide and support the moving platen, so inspect for damage and uneven wear. These ten parts interact, and a fault in one can affect several others. A practical purchase review includes maintenance records, sample runs, and measurements under operating conditions. Not every machine needs new components. Replacing a part without diagnosing the cause can repeat the problem.
Top 10 Plastic Injection Machine Parts Buyers Should Know
The chart groups ten common machine components by the system they belong to. Counts show the components included in this overview, not market share or failure rates.
Injection unit (6): hopper, screw, barrel, nozzle, check ring, and heater bands. Clamping unit (3): moving platen, tie bars, and toggle mechanism. Hydraulic power system (1): hydraulic pump. Part designs and configurations vary by machine.
How to Choose Compatible, Reliable Machine Parts
Choosing compatible, reliable injection machine parts starts with measurements, not catalog photos. Match the machine’s model and revision, then verify dimensions, material, pressure rating, temperature range, and connection type. A screw or nozzle that looks correct may still create uneven melt flow or leakage. Check the machine manual and compare worn parts with drawings or measured samples. Fit matters.
Reliability also depends on operating conditions. Record resin type, cycle frequency, and typical barrel temperature before selecting heaters, seals, screws, or check rings. Grand View Research estimated the global injection molding machine market at USD 10.4 billion in 2022 and projected 4.5% annual growth from 2023 to 2030. That market estimate is not a parts-quality rating, but it reflects a large, evolving equipment base where fit and serviceability matter. ISO 20430:2020 sets safety requirements for injection molding machines; buyers should also check that replacement parts preserve the machine’s specified safety functions. An overlooked detail: older machines may have undocumented revisions, so compatibility can remain uncertain until checked.
Tips: Keep a parts log with dimensions, material, and installation date. Ask suppliers for drawings and test records, then inspect critical fits before production. A quick fit check helps, but it cannot replace a controlled trial.
Related Posts
-
2026 Top Injection Machine Parts Suppliers Worldwide
-
How to Identify Parts of Injection Moulding Machine?
-
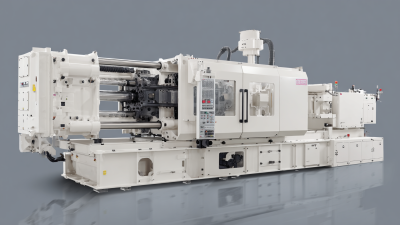
Understanding the Essential Functions of Plastic Injection Machine Parts in Modern Manufacturing
-
Best Plastic Injection Machine Parts for Global Buyers?
-
Top 10 Injection Molding Machine Mold Manufacturers
-
How to Optimize Your Production Process with Injection Molding Machine Mold
Submit a quote request or book a design consultation
Plastimold Products is an end-to-end product development and manufacturing team. We provide product design, engineering, prototyping, tooling, plastic injection molding, assembly, packaging and fulfillment. We work with any size company from start-ups to enterprises from all around the world.
I have a product I want to manufacture
I have a product that is already designed and now needs to be manufactured.
I need a manufacturer to optimize my product for injection molding, help choose the correct material, and manage the product production.
I have tooling that I want to transfer or modify, or I need to produce new tooling.
I need design and engineering support
I have a product concept that I want to be designed and brought to market.
I have a product that needs to be reviewed, improved or DFM’ed.
I am looking for a manufacturer to provide an end-to-end solution, from design and development to inventory, marketing, and sales.
©2022 Plastimold Products - Privacy policy - Terms and Conditions